Featured OEM & ODM Cookware Catalog
High-performance encapsulated bottom & tri-ply woks, frying pans, and stockpots engineered for induction efficiency and heat retention.
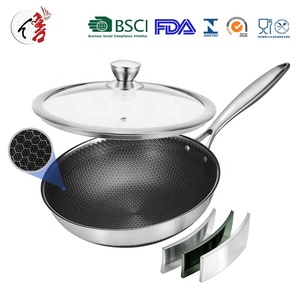
304 Thickened Tri-ply Stainless Steel Honeycomb Wok Non-Stick Pan
Contact Us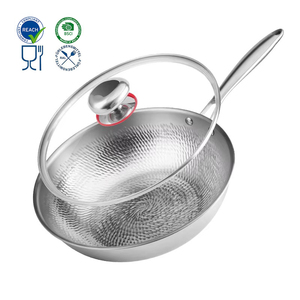
TriPly Stainless Steel Titanium Non Stick Fry Wok Pan with Lid
Contact Us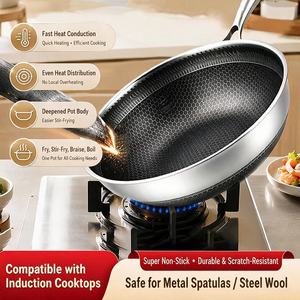
High-Quality Non-Stick Stainless Steel 304/316 18L Cookware
Contact Us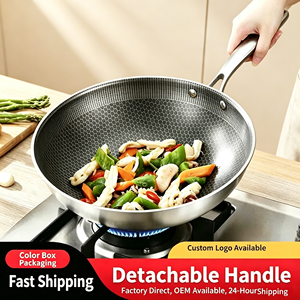
Even Heating Honeycomb Wok Pan Riveted Handle 30/32/34cm
Contact Us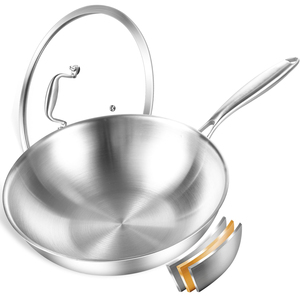
Good Quality Tri-Ply Stainless Steel Wok Durable Cookware Pan
Contact Us
Triply Stainless Steel Woks Stir-Fry Pan with Helper Handles
Contact Us
High Quality 304 Stainless Steel Honeycomb Wok Glass Lid
Contact Us
Premium Thick Bottom 316 SS Double Sided Non-Stick Wok
Contact UsIndustry Whitepaper: Capsule Bottom Cookware Engineering
A B2B Buyer's Guide to Encapsulated Disc Manufacturing, High-Impact Friction Bonding, and Thermal Efficiency Standards
In modern commercial and residential kitchenware manufacturing, the structural engineering of cookware bottoms directly dictates thermal efficiency, energy consumption, and product longevity. As global procurement standards transition toward energy-efficient induction cooking, custom OEM capsule bottom stainless steel cookware has emerged as the industry benchmark for brand owners, hotel supply distributors, and retail chain buyers.
A standard single-ply stainless steel vessel suffers from inherently low thermal conductivity (approximately 15 W/m·K). To overcome hot spots and thermal distortion, specialized OEM manufacturers utilize multi-layer encapsulation technology. This process bonds a high-conductivity aluminum core between an inner food-contact stainless steel layer and an outer magnetic induction base.
Inner Layer: Food-Grade SS304/SS316
Ensures chemical inertness, superior corrosion resistance, and non-reactive cooking surfaces compliant with EU LFGB and US FDA 21 CFR standards. SS316 offers added molybdenum for high-saline commercial environment resistance.
Core Layer: Pure Aluminum (1050/1100)
Featuring a high thermal conductivity rating of ~205 W/m·K, the pure aluminum core thickness ranges from 3.0mm to 7.0mm. It rapidly distributes heat laterally, eliminating hot spots and preventing scorching.
Outer Layer: Magnetic SS430 (18/0)
Engineered with high magnetic permeability to maximize energy transfer on electromagnetic induction hobs, while remaining fully compatible with conventional gas, electric, and ceramic stovetops.
The High-Impact Friction Bonding Process vs. Traditional Brazing
The structural integrity of a capsule bottom cookware piece depends entirely on the bonding process used to join the disc layers. Older manufacturing methodologies relied on flux-brazing, which created microscopic air voids, reduced thermal transfer efficiency, and frequently led to bottom delamination under thermal shock.
Our state-of-the-art OEM production line utilizes High-Impact Friction Pressing Technology (2,000 to 3,500 Tons of hydraulic force). Under intense pressure and friction-generated heat, the metals interlock at a molecular level without chemical fluxes. This yields a seamless 100% solid bottom encapsulation that guarantees:
- Zero internal air pockets, maximizing thermal transfer velocity.
- Resistance to disc detachment even when subjected to repeated thermal shock (heating to 300°C followed by immediate water quenching).
- Compliance with DIN 44550 thermal concavity standards, keeping the bottom flat during high-heat expansion for optimal contact with induction glass hobs.
| Technical Parameter | Standard Encapsulated Disc | Heavy-Duty Impact-Bonded Bottom | Full Clad Tri-Ply (Wall + Base) |
|---|---|---|---|
| Hydraulic Pressing Force | 800 – 1,200 Tons | 2,500 – 3,500 Tons | Continuous Roll Bonding |
| Aluminum Core Thickness | 1.5mm – 2.5mm | 3.5mm – 6.5mm (Heavy Gauge) | 1.5mm – 2.0mm |
| Delamination Thermal Shock Risk | Moderate under high commercial use | Zero (Molecular Bond Guarantee) | None |
| Induction Efficiency Rate | 82% – 86% | 94% – 97% | 88% – 92% |
| Unit Cost Economy for OEM Sourcing | Low | Optimal High Value / Performance Ratio | High Premium |
Future Global Procurement Trends in Cookware
Market dynamics, sustainability mandates, and technical innovations shaping B2B sourcing decisions over the next decade.
1. Strict EU & US Energy Efficiency Directives
Governments worldwide are accelerating eco-design policies targeting home appliances and cookware. Procurement officers are shifting toward thick-core capsule bottoms that heat up 30% faster, drastically reducing gas and electricity consumption.
2. Hybrid Etched Non-Stick Surfaces
Commercial buyers are replacing fragile traditional coatings with laser-etched stainless steel honeycomb matrices. This hybrid construction protects PFOA-free coatings beneath raised stainless steel pillars, allowing metal utensil usage without surface degradation.
3. Supply Chain Traceability & Material Audits
Enterprise buyers now demand mill test certificates (MTC) verifying exact nickel and chromium ratios in stainless steel coils. Standardized XRF spectro-analysis reporting is becoming a prerequisite for container clearance.
Enterprise Capabilities & OEM Advantage
Why leading global kitchenware brands partner with Adil Stainless Steel for custom capsule bottom production.
Established in 2006 in Gujranwala—Pakistan’s premier manufacturing hub for high-grade steel and kitchenware—Adil Stainless Steel has built an internationally recognized OEM/ODM infrastructure serving importers, supermarket chains, and B2B distributors across more than 10 countries.
Full Vertical Integration
From raw stainless steel coil slitting and deep-drawing pressing to hydraulic impact bonding, automatic surface polishing, and custom packaging—every production stage takes place under strict internal Quality Control (QC).
10,000+ Product Portfolio & Tooling Library
Our factory maintains an extensive archive of ready molds for cookware sets, pressure cookers, steamers, stock pots, and hot pots, significantly reducing tooling costs and accelerating time-to-market for private label clients.
ISO Certified & International Compliance
Operating under ISO 9001 certified quality management systems, our products comply with strict international food-grade standards, ensuring smooth customs clearance across the EU, Middle East, Africa, and Americas.
Bespoke Private Labeling & Custom Packaging
We provide turnkey OEM services including laser logo etching, custom handle design (cast stainless steel, hollow cool-touch, or silicone-molded), color gift box printing, and export master carton drop-testing.
Frequently Asked Questions (FAQ) for B2B Buyers
Essential technical, logistics, and manufacturing insights for procurement managers and global sourcing agents.
Q1: What is the main difference between capsule bottom cookware and full-clad tri-ply cookware?
Capsule bottom cookware features a multi-layer disc bonded exclusively to the base of a single-ply stainless steel body. This concentrates heat distribution where it is needed most while keeping overall vessel weight and manufacturing costs economic. Full-clad tri-ply cookware extends the three-layer aluminum-core material up the entire sidewall to the rim. Capsule bottom cookware provides superior cost-to-performance efficiency for large-capacity stockpots, pressure cookers, and high-volume commercial cookware lines.
Q2: How do you prevent the encapsulated bottom disc from separating over time?
Disc detachment occurs when traditional brazing or low-tonnage pressing leaves microscopic voids. We utilize 2,500+ ton high-impact friction bonding. Under this force, the aluminum metal liquefies briefly at the interface, causing the metallic lattices of the SS304 body, aluminum disc, and SS430 base plate to interlock molecularly. Our cookware undergoes rigorous thermal shock testing (heated to 300°C and cold-water quenched) to ensure zero delamination.
Q3: Which stainless steel grades are used for your OEM manufacturing?
We primarily offer food-grade AISI 304 (18/8) and AISI 316 (18/10) for internal cooking surfaces to guarantee maximum rust resistance and non-reactivity with acidic foods. The outer encapsulation plate uses magnetic AISI 430 (18/0) stainless steel to ensure high responsiveness on induction hobs.
Q4: What is the minimum order quantity (MOQ) for custom OEM branding?
Our standard Minimum Order Quantity for custom logo etching and customized color packaging starts at 500 sets (or 1,000 individual pieces) per size, depending on vessel specifications. We also offer flexible MOQ arrangements for trial containers combining multiple product catalog SKUs.
Q5: Can you manufacture cookware according to our specific design drawings or sample?
Yes. Our in-house engineering center offers complete ODM services, including 3D CAD modeling, CNC mold die creation, rapid prototyping, and sample validation prior to mass production. Mold tooling timelines typically range from 15 to 25 days.
Q6: How is the induction base flatness guaranteed during production?
Cookware bases naturally expand when heated. We engineer a precise concave tolerance (in accordance with international standard DIN 44550) during bottom stamping. When heated on an induction cooktop, the thermal expansion flattens the bottom completely, maintaining maximum magnetic contact and preventing wobbling or energy loss.
Partner with a Premier Capsule Bottom Cookware Manufacturer
Looking for dependable OEM/ODM manufacturing, high-impact bonding quality, and competitive factory-direct pricing? Speak directly with our engineering and export sales team.